Product brief description
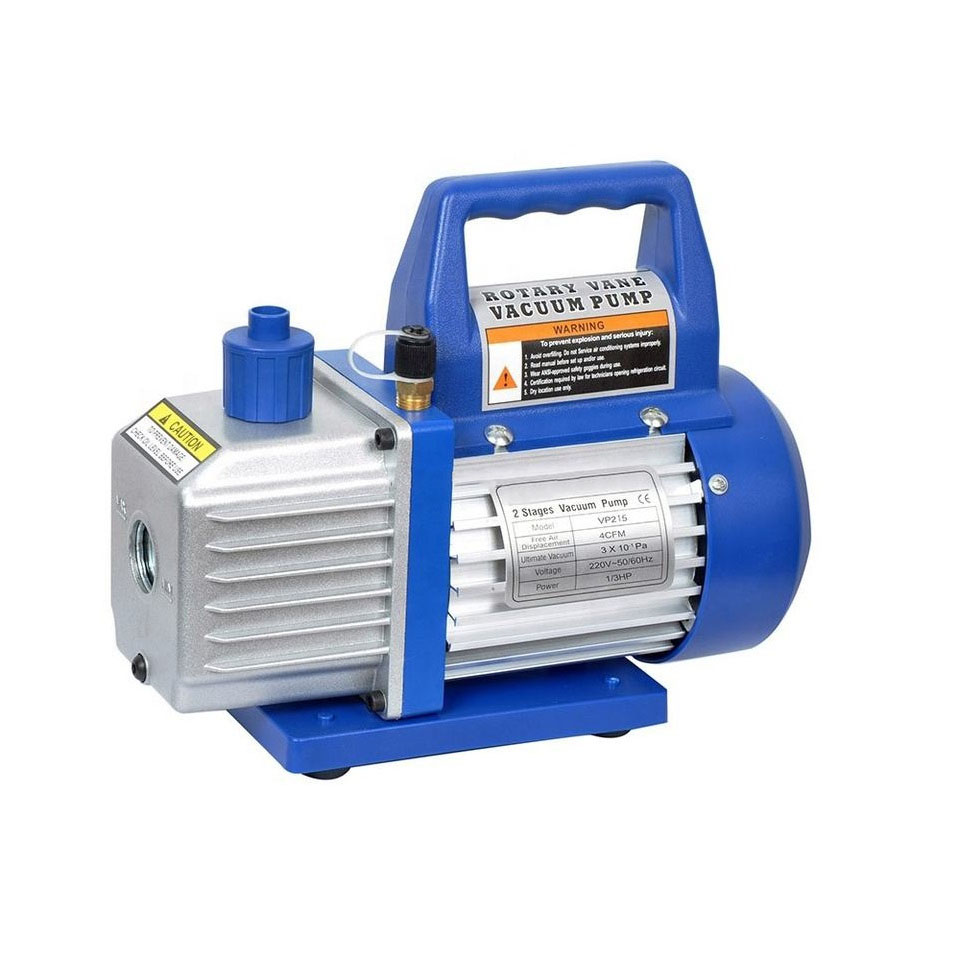
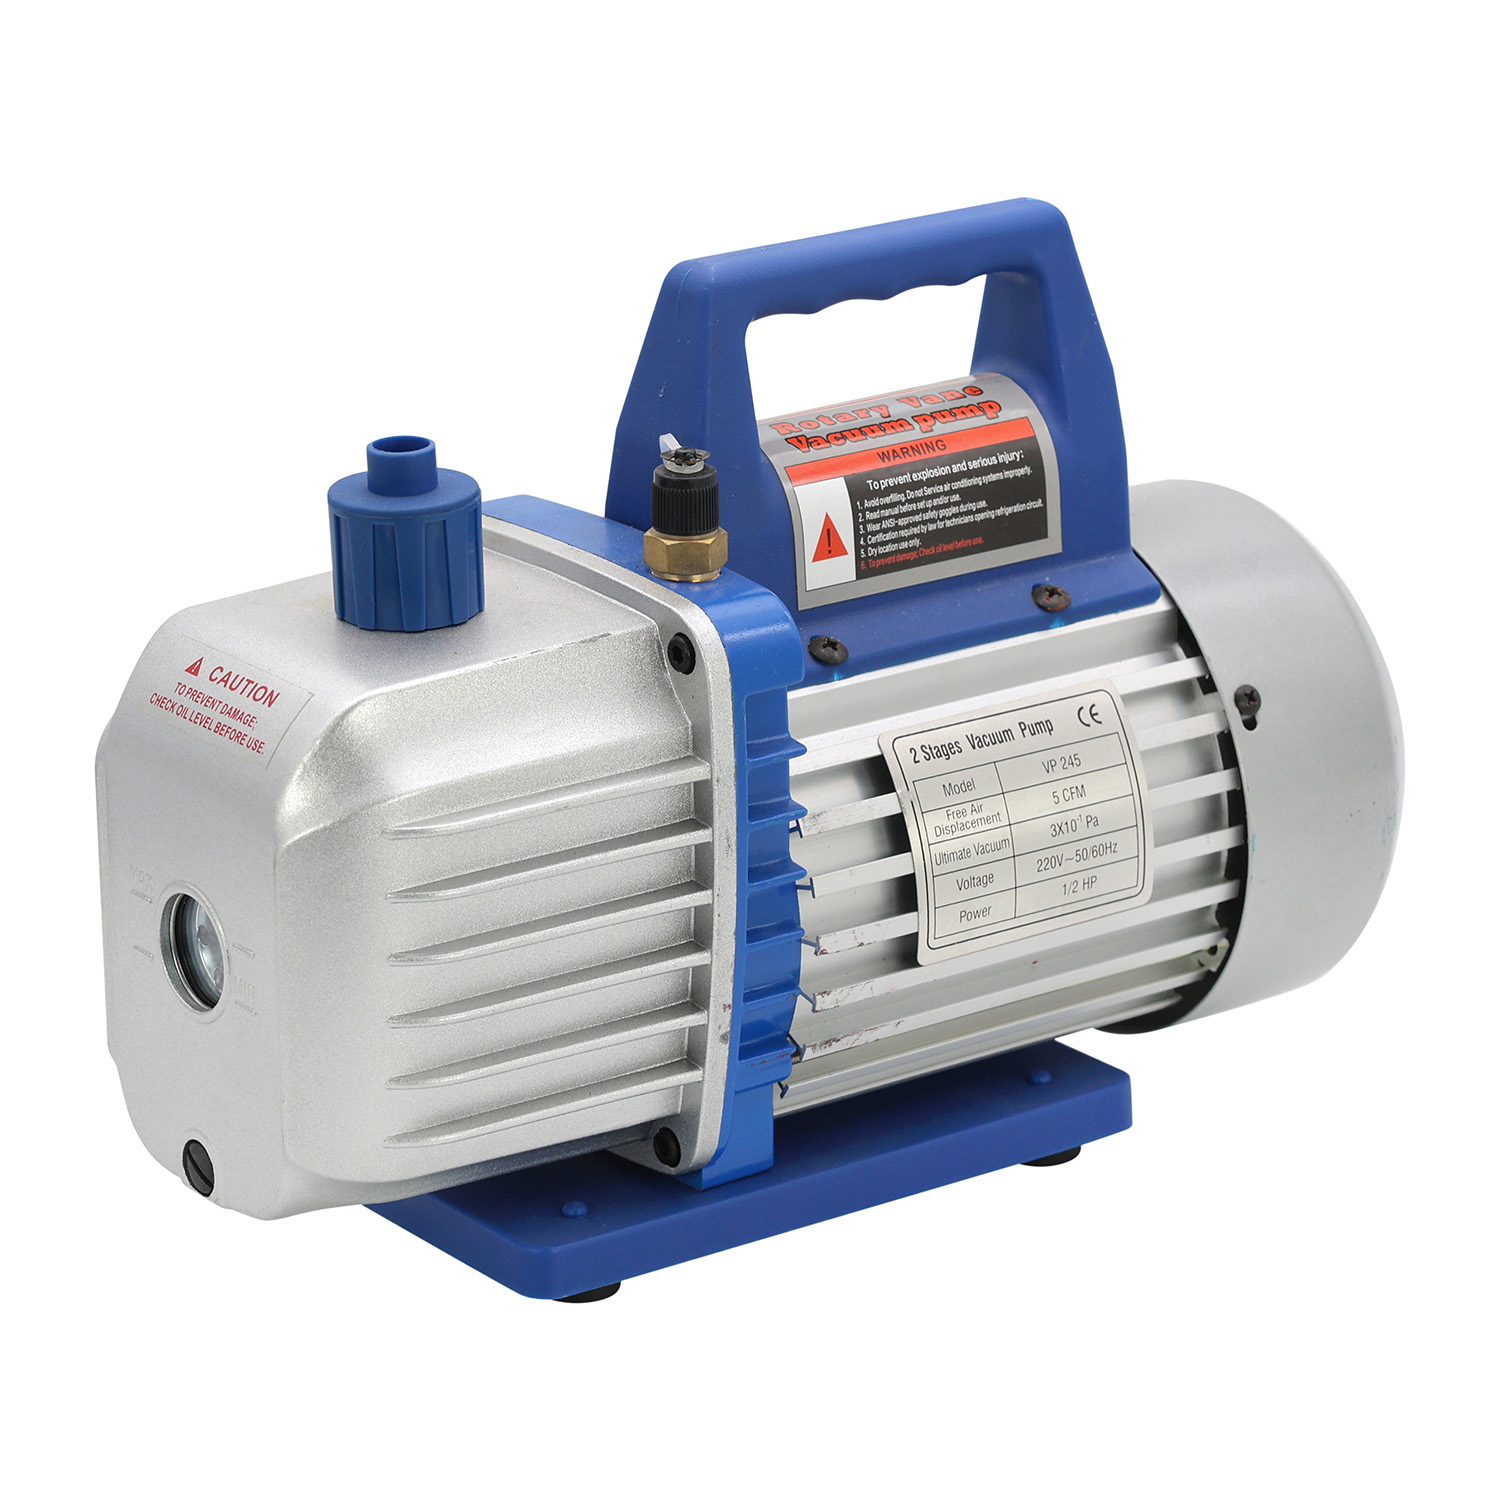
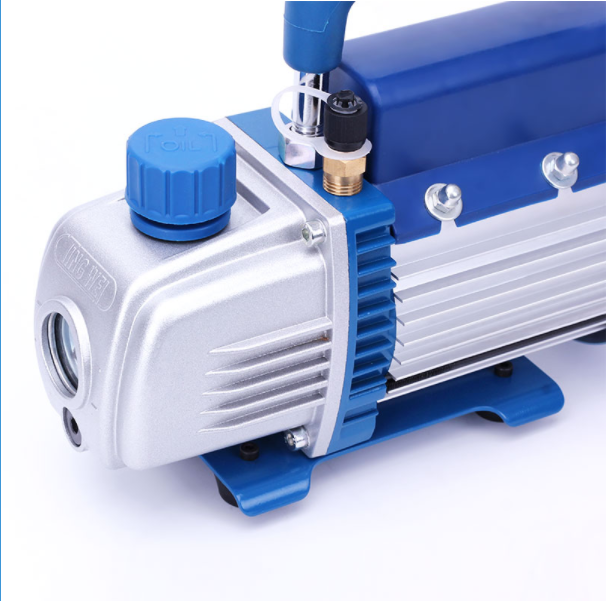
Professional Rotary Vane Vacuum Pump is a dedicated electric device for HVAC and refrigeration system installation and routine maintenance. Supporting single-stage and double-stage working modes, this vacuum pump delivers fast pumping speed, ultra-high vacuum performance and low-noise stable operation. Built with oil anti-backflow valve and overheat protection structure, it effectively prevents pipeline contamination and equipment burnout. It efficiently removes residual air, moisture and non-condensable gases inside refrigeration pipelines for vacuum degassing, pipeline drying and pressure holding tests. Compact, portable and durable, it is an essential professional tool for residential air conditioner repair and commercial refrigeration engineering maintenance.
Product detailed description
High Efficiency Rotary Vane Vacuum Pump for Professional HVAC Refrigeration Maintenance
Our vacuum pump is an upgraded professional electric vacuumiing device tailored for global HVAC engineering teams and refrigeration maintenance industries. In refrigeration system installation and daily maintenance, pipeline vacuuming is one of the most critical pretreatment processes. A large amount of air, water vapor and impurity gas will remain inside newly installed or overhauled refrigeration pipelines. If these gases are not completely discharged, they will cause ice blockage in capillary tubes, reduced refrigeration efficiency, increased system operating pressure, accelerated pipeline oxidation and even compressor burnout, leading to frequent equipment failures and shortened service life. Ordinary low-quality vacuum pumps have obvious defects such as slow pumping speed, low ultimate vacuum degree, easy oil backflow, severe heating and loud noise, which cannot meet the high-standard vacuuming requirements of modern high-precision refrigeration systems. Our optimized single and double stage vacuum pumps solve all industry pain points, delivering fast, thorough, stable and safe vacuuming effects for various refrigeration equipment.
Advanced Rotary Vane Structure & Ultra-High Pumping Efficiency
This vacuum pump adopts precision rotary vane compression principle and internal eccentric rotor structure. The high-speed rotating rotor drives the rotary vane to compress and discharge gas continuously, realizing rapid extraction of internal air and moisture in refrigeration pipelines. Compared with ordinary ordinary vacuum pumps with low displacement and slow exhaust speed, our equipment has larger pumping volume and higher working efficiency, which can quickly complete vacuuming work in a short time and greatly improve on-site construction progress. The internal precision-fit rotor and cylinder body are processed by high-precision CNC machining, with tight matching clearance and no air leakage during operation, ensuring stable and continuous vacuuming capacity without pressure attenuation, effectively improving the ultimate vacuum degree of the system.
Unique Anti-Backflow Protection Design & Safe Operation
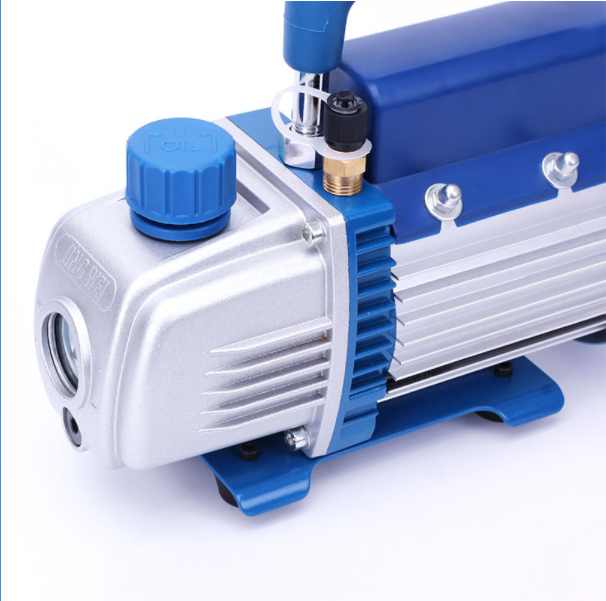
Equipped with professional built-in oil anti-backflow valve and one-way pressure maintaining structure, this vacuum pump fundamentally solves the common problem of vacuum pump oil backflow pollution. When the equipment stops working or the pipeline pressure rebounds, the one-way valve automatically closes to lock the pipeline vacuum degree and prevent vacuum pump oil from flowing back into the refrigeration pipeline to cause oil pollution and pipeline blockage. This core protection design effectively avoids secondary pollution of clean refrigeration systems, protects pipeline cleanliness and refrigerant purity, and ensures the stable operating efficiency of air conditioning and refrigeration units. It completely solves the maintenance hidden danger of ordinary vacuum pumps that are prone to oil backflow and cause equipment failure.
Low Noise & Efficient Heat Dissipation System
The vacuum pump is equipped with a high-quality silent motor and optimized fan blade structure, which effectively reduces operating vibration and wind resistance noise. The overall operating sound is low, meeting the noise standard of indoor construction and commercial engineering environments. The body adopts multi-channel heat dissipation structure and thickened heat dissipation fin design, which can quickly export the high temperature generated by long-term high-load operation. It avoids equipment overheating, power attenuation and thermal shutdown failure during continuous vacuuming operation, realizing long-term stable non-stop work and greatly improving the continuous working capacity of engineering construction.
Stable Motor Performance & Durable Industrial Quality
Built-in high-power pure copper motor features strong power, fast startup speed and stable output power, with no stalling or insufficient pumping power under high-load working conditions. The pure copper coil has strong conductivity, low heat generation and long service life, which is more durable than ordinary aluminum coil motors. The whole machine adopts thickened metal shell and anti-vibration base design, with strong compression resistance, drop resistance and structural stability. All core components have passed strict industrial aging tests and continuous operation tests, adapting to long-term high-frequency outdoor and indoor engineering use, with low failure rate and long service life.
Single & Double Stage Optional & Full-Scenario Adaptation
We provide single-stage and double-stage two mainstream configurations to meet different engineering needs. Single-stage vacuum pump is cost-effective and efficient, suitable for conventional household air conditioner installation, small refrigeration equipment maintenance and daily vacuuming work. Double-stage vacuum pump adopts secondary supercharging structure, with higher ultimate vacuum degree and more thorough degassing effect, which is specially used for high-standard commercial central air conditioning, large cold storage units, heat pump equipment and precision refrigeration system vacuuming. It can effectively remove micro moisture and residual gas in the pipeline, ensuring the refrigeration system operates with high efficiency and low energy consumption for a long time.
Portable Design & Wide Industry Compatibility
The vacuum pump adopts lightweight integrated body design with compact structure and portable size, which is convenient for mobile carrying, vehicle-mounted transportation and on-site outgoing construction. It is widely compatible with all mainstream refrigerants and refrigeration systems such as R22, R134a, R410A and R32, covering household air conditioners, refrigerators, freezers, commercial display cabinets, constant temperature and humidity equipment, cold storage units and central air conditioning systems. It supports vacuum degassing, pipeline drying, pressure holding test and air extraction before refrigerant filling, meeting full-process professional maintenance needs of HVAC refrigeration engineering.
Product Specifications
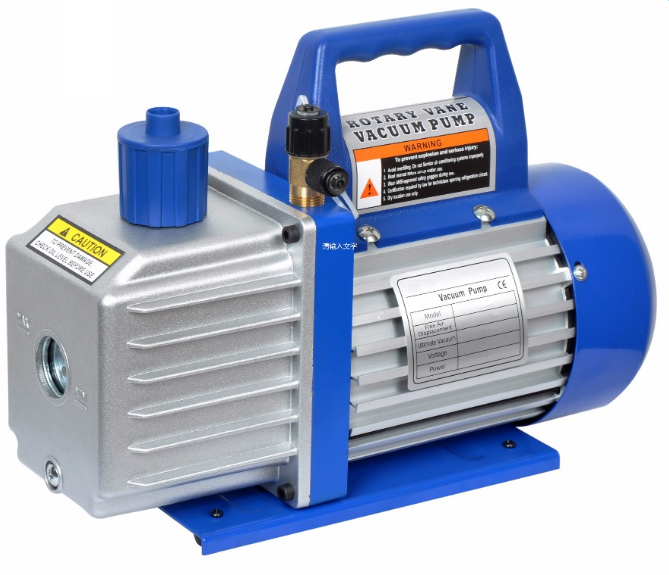
1.Stage Vacuum Pump
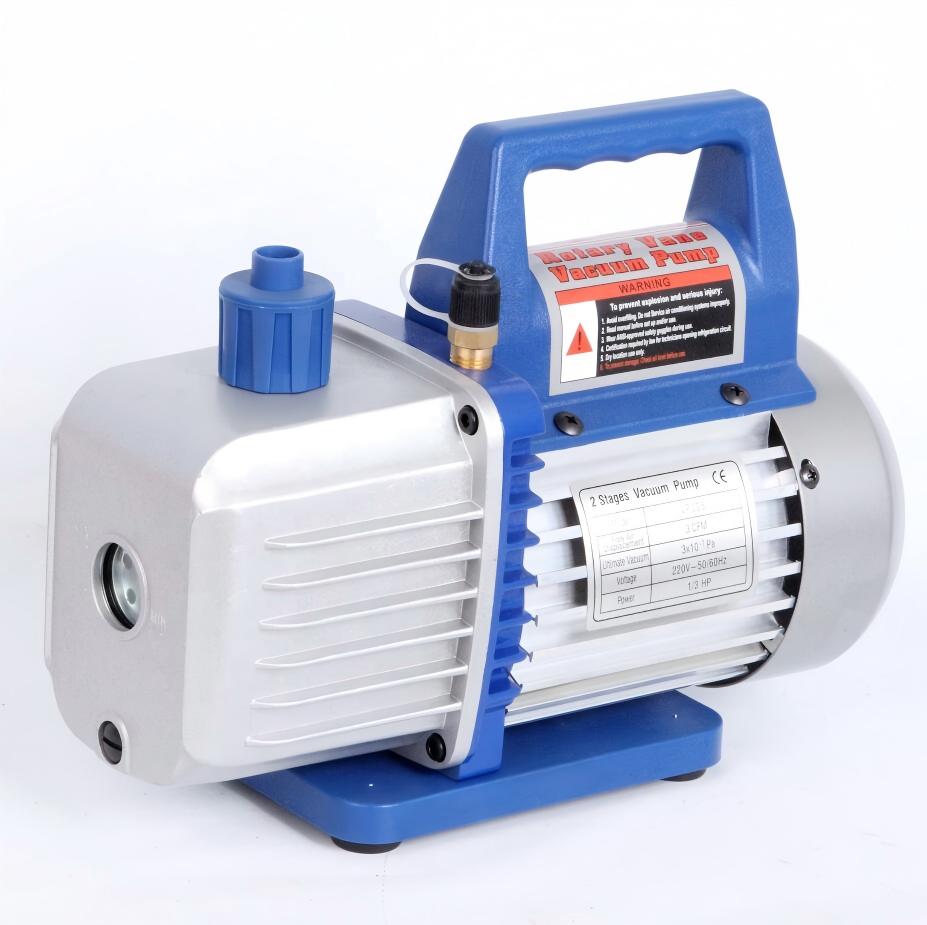
2.Stages Vacuum Pump
FAQ
Q1: What is a vacuum pump used for?
A: Vacuum pump is a core electric tool for HVAC refrigeration maintenance. It is mainly used to extract air, moisture and non-condensable gas from refrigeration pipelines, complete system vacuum degassing and pipeline drying before refrigerant filling, ensuring stable and efficient operation of refrigeration equipment.
Q2: What is the difference between single-stage and double-stage vacuum pumps?
A: Single-stage vacuum pump is cost-effective for daily household and small commercial equipment vacuuming. Double-stage model adopts secondary supercharging structure with higher vacuum degree and cleaner degassing effect, suitable for high-standard commercial units, cold storage and precision HVAC systems.
Q3: Does this vacuum pump have oil backflow protection?
A: Yes. Built-in professional one-way anti-backflow valve, it can effectively prevent vacuum pump oil from flowing back into the refrigeration pipeline when stopping operation, avoiding pipeline pollution, blockage and equipment failure caused by oil backflow.
Q4: Is the pumping speed fast and the vacuum degree high?
A: Absolutely. Adopting precision rotary vane structure and pure copper high-power motor, it features fast pumping speed and low residual air volume. The high-end double-stage model can reach ultra-high ultimate vacuum, completely meeting high-standard refrigeration engineering requirements.
Q5: Can it work continuously for a long time?
A: Yes. Equipped with efficient heat dissipation system and overheat protection function, the vacuum pump can operate stably for a long time without overheating and power attenuation, adapting to continuous high-load operation of on-site engineering construction.
Q6: Is the operation noise loud?
A: No. Optimized silent motor and fan structure reduce operating vibration and wind noise effectively. The overall noise is low, suitable for indoor household maintenance, commercial shopping malls and office building engineering construction scenarios.
Q7: What refrigeration equipment is it compatible with?
A: It is widely applicable to all HVAC refrigeration equipment, including household air conditioners, refrigerators, freezers, commercial display cabinets, cold storage units, heat pump equipment and central air conditioning systems, compatible with all mainstream refrigerants.
Q8: How about the packaging and transportation?
A: Each vacuum pump is individually packed with shockproof, dust-proof and moisture-proof packaging to protect the motor and internal precision components. Bulk orders use reinforced export cartons, supporting long-distance sea freight and global wholesale and engineering orders.
 ONLINE


 EN