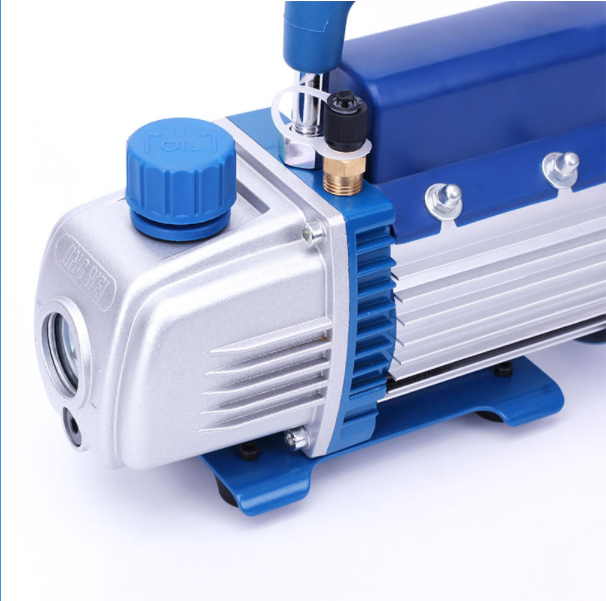
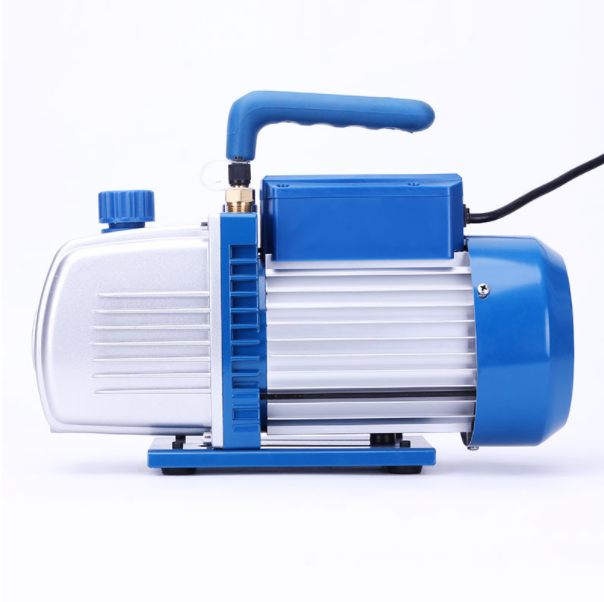
Refrigeration Vacuum Pump | 100 L/min, 0.3 Pa Deep Vacuum

All Categories
High-Performance Refrigeration Vacuum Pump for Reliable Cooling Systems

High-Performance Refrigeration Vacuum Pump for Reliable Cooling Systems

Suzhou Eletek Inc. is a professional manufacturer of household refrigeration appliances, and we are proud to introduce our advanced refrigeration vacuum pump. This essential tool is designed for HVAC technicians and refrigeration engineers who demand efficiency and durability. Whether you are evacuating moisture and air from refrigeration circuits or performing maintenance on air conditioners, freezers, or cold rooms, our vacuum pump ensures a deep and reliable vacuum. With a robust design built to withstand rigorous use, it features high pumping speed, low noise, and oil-free operation options to suit various applications. Our pump is rigorously tested in our professional laboratory to meet international standards, ensuring consistent performance. We understand that any leak or residual moisture can compromise the cooling efficiency, so our pump’s precision engineering guarantees a thorough evacuation process, extending the lifespan of refrigeration systems.
Get A Quote
Advantages of the product

High Pumping Speed and Efficiency

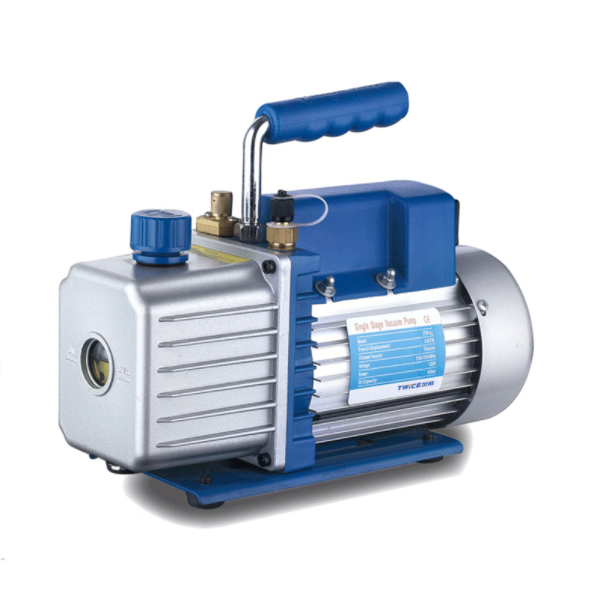
Our refrigeration vacuum pump is engineered with a high-flow design that ensures rapid evacuation of air and moisture from any refrigeration system. With a pumping speed of up to 100 liters per minute, it significantly reduces the time needed to reach the required vacuum level, increasing your productivity. The pump uses a two-stage rotary vane mechanism that generates an ultimate vacuum of up to 0.3 Pa, ensuring a thorough evacuation that prevents future system failures. This high efficiency is crucial for maintaining the integrity of the cooling circuit and maximizing the performance of the compressor. Whether you are working on a small refrigerator or a large cold room, this pump adapts to the volume and delivers consistent performance. Additionally, the efficient motor is designed to consume less energy while providing maximum output, reducing operational costs. With a built-in thermal protection system, the pump automatically shuts off to prevent overheating, ensuring durability.

Durable Construction for Long-Lasting Performance

The refrigeration vacuum pump is built with a heavy-duty aluminum alloy body that resists corrosion and withstands the rigors of daily use. The rotary vanes are made from high-grade carbon composite materials, which are self-lubricating and resistant to wear, ensuring a long service life. The pump’s shaft is precision-balanced to minimize vibration, reducing stress on internal components and extending the overall lifespan. A rugged carrying handle and non-slip rubber feet provide stability during operation, while the compact design allows for easy transportation and storage. The pump is also equipped with an anti-backflow valve that prevents oil from returning to the system, protecting your equipment from contamination. All external parts are coated with a scratch-resistant powder finish, maintaining an attractive appearance even after years of use. Our production process follows lean management principles, ensuring consistent quality in every unit. We have also incorporated a large-vi

User-Friendly Design and Easy Maintenance

We have designed our refrigeration vacuum pump with the end-user in mind, ensuring that it is easy to operate, even for technicians with minimal experience. The clear analog vacuum gauge provides precise readings, and a simple control valve allows for quick adjustments. An ergonomic handle ensures comfortable carrying, while the lightweight construction (only 12 kg) reduces fatigue during transport. The pump features a tool-free oil drain port and a convenient oil fill cap, making oil changes straightforward and mess-free. The intake port is equipped with a standard 1/4-inch SAE fitting that connects to most refrigeration hoses, and a spare connection port allows for flexibility. We also provide comprehensive user manuals in multiple languages, ensuring clear guidance for international users. The maintenance steps are clearly outlined, and all internal components are accessible for cleaning or replacement. For added convenience, the pump includes a carrying case option and spare parts

Related products

Refrigeration vacuum pump technology is critical in the installation, servicing, and repair of refrigeration and air conditioning systems. The primary function of such a pump is to remove air and moisture from the sealed system before charging refrigerant. If moisture remains, it can freeze and cause blockages in the expansion valve, while air can increase condensing pressure and reduce cooling capacity. A high-quality vacuum pump, like the Eletek EVP-100, ensures that the system is thoroughly evacuated to a level where moisture is vaporized and removed, preventing future failures. The process involves connecting the pump to the system via service valves and running it for a specified time, often using a micron gauge to measure the vacuum level. A good pump should be capable of pulling a vacuum to at least 500 microns, ideally below 200 microns, to ensure complete dehydration. Our pump achieves this with its two-stage rotary vane mechanism, which uses an oil seal to prevent back leakage and maintain deep vacuum. It’s essential to change the pump oil regularly to maintain performance, as contaminated oil can reduce its efficiency. We recommend using the specific high-grade vacuum pump oil, which we also supply. When operating the pump, ensure proper ventilation and follow safety guidelines to avoid oil vapors. Our EVP-100 includes a gas ballast valve that helps extend oil life by allowing moisture vapor to escape before it condenses in the oil, a feature that is especially useful in humid climates. By understanding the importance of a good vacuum, technicians can deliver more reliable service, reduce callbacks, and extend the life of compressors. Investing in a dependable vacuum pump is therefore indispensable for any professional. At Eletek, we are dedicated to providing education and high-quality tools to help our customers achieve excellence in their work, aligning with our vision of being a good tool for a better life.

Frequently Questions

What is the optimal vacuum level for a refrigeration system?

The optimal vacuum level for a refrigeration system typically depends on the manufacturer’s specifications, but as a general rule, a deep vacuum of 500 microns or below is recommended to ensure complete removal of moisture and air. For systems with POE oils, it is crucial to achieve below 500 microns to prevent acid formation and moisture-related issues. Ideally, a vacuum of 200 microns or lower is considered excellent and ensures a dry and clean system. The Eletek refrigeration vacuum pump can achieve an ultimate vacuum of 0.3 Pa, which is equivalent to 2.25 microns, well beyond the standard requirement. However, the final vacuum reading will also depend on the system size, ambient conditions, and the absence of leaks. To accurately measure the vacuum, use a reliable micron gauge connected directly to the system. It’s also advisable to perform a vacuum decay test to ensure the system holds the vacuum, indicating no leaks. When using our pump, we recommend pulling a vacuum for at least
The frequency of oil changes depends on usage and operating conditions. As a general recommendation, change the oil after every 50 hours of operation or at least once a month for daily professional use. If you are using the pump in humid environments, you may need to change the oil more frequently because moisture can contaminate the oil and reduce its effectiveness. Signs that the oil needs changing include a milky appearance, a distinct odor, or the pump taking longer to reach the desired vacuum. Eletek’s EVP-100 has a large oil reservoir and a viewing window to help you visually inspect the oil condition. We recommend using a high-grade vacuum pump oil with low vapor pressure to maintain optimal performance. When changing the oil, ensure the pump is warm to promote drainage, but not hot. Follow the manufacturer’s instructions in the manual, and always dispose of used oil properly. Regular oil changes not only extend the pump’s lifespan but also ensure consistent vacuum performance.
While a refrigeration vacuum pump is designed specifically for HVAC and refrigeration systems, it can technically be used for other applications that require a deep vacuum, such as vacuum packaging, degassing, or laboratory processes. However, there are important considerations. Refrigeration vacuum pumps use oil sealing, which means the vacuum chamber is not completely oil-free; there is a tiny amount of oil vapor that can contaminate certain processes. For food vacuum packaging, you would need to use a vacuum pump with food-grade oil and an appropriate filter, and even then it may not be suitable because the pump’s oil vapor can affect taste. Also, the pump is designed to handle refrigerant gases and moisture, but not fine powders or corrosive chemicals. If you intend to use it for other purposes, ensure you install a vacuum trap or filter to protect the pump and the application. It’s also essential to verify that the vacuum level is compatible with your needs. The Eletek EVP-100 ach
The main difference lies in the number of compression stages. A single-stage vacuum pump uses one compression stage and can typically achieve an ultimate vacuum of about 20-50 microns. A two-stage pump, like the Eletek EVP-100, uses two stages in series, allowing it to achieve a much deeper vacuum, down to 2-5 microns. This deeper vacuum is essential for removing all moisture and air from refrigeration systems, especially those with newer refrigerants like R-410A or R-32, which are more sensitive to moisture. Two-stage pumps are also more efficient at higher altitudes where atmospheric pressure is lower. For professional refrigeration work, a two-stage pump is highly recommended because it ensures a thorough evacuation, reducing the risk of system failures. The trade-off is that two-stage pumps are generally more expensive and slightly larger, but they provide superior performance. In our EVP-100, the two stages are compactly integrated, and the pump’s pumping speed and vacuum capacity
Proper maintenance is key to extending the life of your refrigeration vacuum pump. First, always use clean, high-quality vacuum pump oil and change it regularly as per the schedule mentioned. After each use, it’s good practice to run the pump for a few minutes with the gas ballast valve open (if available) to purge any moisture from the oil. This prevents oil contamination and extends its life. Clean the exterior of the pump and check for any loose fittings or seals. Periodically inspect the intake filter or screen to ensure it’s not clogged. If your pump has a replaceable exhaust filter, replace it when it becomes saturated. Also, ensure that the pump is stored in a dry, clean environment when not in use. Before storage, cap the intake to prevent dust from entering. Regularly check the motor and electrical connections for any signs of wear. In case of any unusual noise or performance issues, refer to the troubleshooting section in the manual. Our Eletek pump is designed for easy acces

Related article

The Importance of Calibrating Refrigeration Tools

22

Jul

The Importance of Calibrating Refrigeration Tools

The Critical Necessity of Precision in Refrigeration Maintenance In the demanding world of HVAC/R service and maintenance, success is measured in increments of degrees and PSI. Facility managers and field technicians often overlook the invisible infl...
View More
Copper Connecting Tube Insulation Requirements

23

Jul

Copper Connecting Tube Insulation Requirements

The Vital Role of Proper Insulation for Thermal Performance Achieving peak efficiency in HVAC and refrigeration systems often relies on the smallest details, where the copper connecting tube plays a fundamental role. These tubes serve as the arteries...
View More
How Air Conditioning Parts Impact System Reliability

20

Aug

How Air Conditioning Parts Impact System Reliability

The Foundation of Industrial and Commercial Climate Control When evaluating the performance of large-scale heating, ventilation, and air conditioning infrastructures, attention frequently drifts toward computerized thermostats or expansive duct desig...
View More

Customer Testimonials

Mark Johnson
Efficient and Reliable Vacuum Pump for HVAC Work

As a professional HVAC technician, I have tested many vacuum pumps, and the Eletek EVP-100 has become my go-to choice. It pulls a strong vacuum quickly, reducing my service time significantly. The build quality is top-notch, and I appreciate the easy-to-read gauge. I’ve used it on both residential and commercial systems, and it never disappoints. The two-stage design ensures that all moisture is removed, leading to fewer callbacks. The compact size makes it easy to carry in my van, and the oil change process is simple. I highly recommend this pump to any technician looking for reliability and efficiency.

Hans Muller
Great Value for Money and Durable

We run a refrigeration repair service in Germany, and we invested in the Eletek vacuum pump after our previous pump failed. This pump has exceeded our expectations. It operates quietly, and the vacuum level is consistently deep. We’ve used it extensively without any issues. The after-sales support from Eletek was excellent, with quick response to our queries. The pump’s robust construction gives us confidence that it will last for years. It’s an affordable yet professional-grade tool that I would recommend to any refrigeration technician.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000
Precision Engineering for Ultimate Vacuum Performance

Precision Engineering for Ultimate Vacuum Performance

The Eletek refrigeration vacuum pump is meticulously engineered to deliver an ultimate vacuum of 0.3 Pa, ensuring the complete removal of air and moisture from any refrigeration system. This level of precision is achieved through a two-stage rotary vane design, which uses high-grade carbon composite vanes that maintain a tight seal over time. The pump’s internal clearances are optimized to minimize back leakage, and a high-capacity oil separator ensures that the exhaust air is free of oil mist. The result is a pump that consistently achieves the deep vacuum required for modern refrigerants, which are susceptible to moisture and non-condensable gases. This precision translates to enhanced system performance, reduced energy consumption, and fewer breakdowns for end-users. By integrating a gas ballast valve and an anti-backflow check valve, the pump safeguards your system from contamination and extends compressor life.
Portable and Space-Saving Design

Portable and Space-Saving Design

Our refrigeration vacuum pump features a compact, lightweight design that is easy to transport to job sites. Weighing just 12 kg and equipped with a ergonomic handle, the pump can be carried effortlessly, even with one hand. Its footprint is smaller than comparable models, making it easy to store in a service van or tool bag. Despite its small size, it does not compromise on performance, offering a high pumping speed of 100 L/min. The inclusion of rubber foot pads reduces vibrations and ensures stability on uneven surfaces, allowing for safe operation. The design also incorporates a carry case option, which provides additional protection during transit. This portability is a key advantage for technicians who need to move between locations frequently. The pump’s intake ports are conveniently located and standard, allowing for quick connection to hoses.
onlineONLINE
email goToTop