High-Performance Refrigeration Vacuum Pump for Reliable Cooling Systems
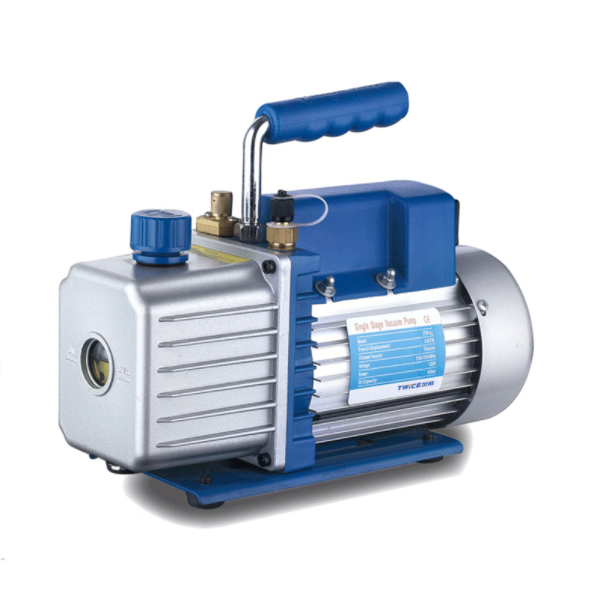
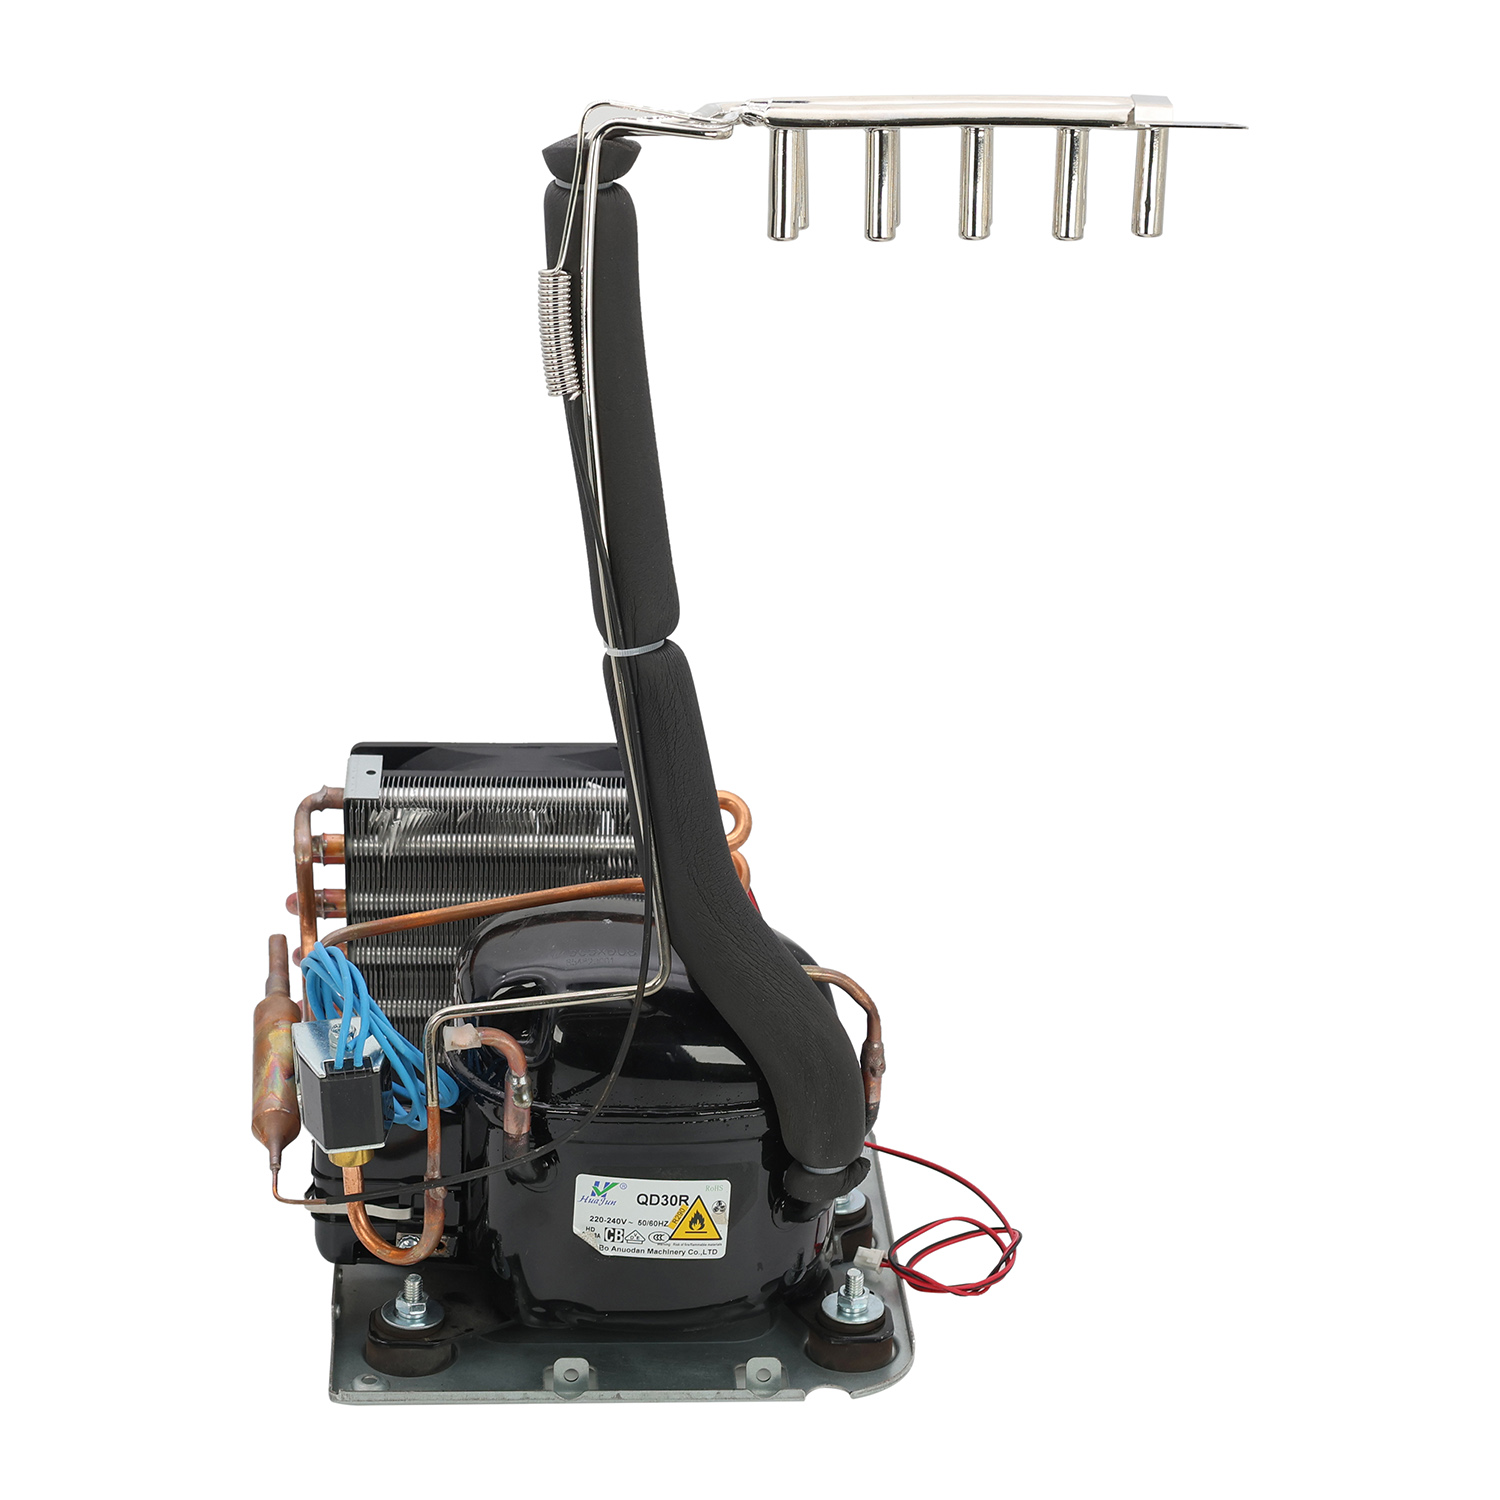
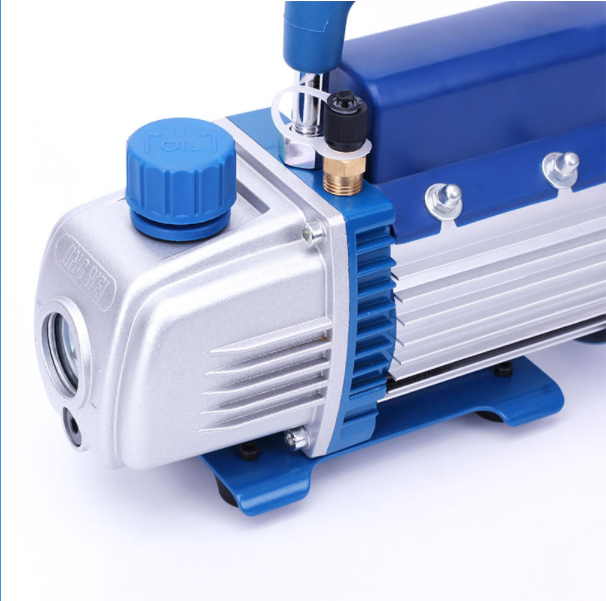
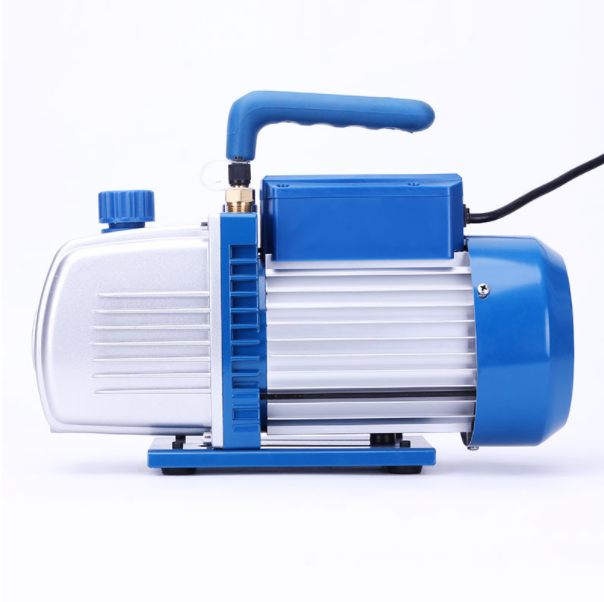
Suzhou Eletek Inc. is a professional manufacturer of household refrigeration appliances, and we are proud to introduce our advanced refrigeration vacuum pump. This essential tool is designed for HVAC technicians and refrigeration engineers who demand efficiency and durability. Whether you are evacuating moisture and air from refrigeration circuits or performing maintenance on air conditioners, freezers, or cold rooms, our vacuum pump ensures a deep and reliable vacuum. With a robust design built to withstand rigorous use, it features high pumping speed, low noise, and oil-free operation options to suit various applications. Our pump is rigorously tested in our professional laboratory to meet international standards, ensuring consistent performance. We understand that any leak or residual moisture can compromise the cooling efficiency, so our pump’s precision engineering guarantees a thorough evacuation process, extending the lifespan of refrigeration systems.
Get A Quote
 EN
 ONLINE

